EN





- Overview
- Main Parameters
- Recommended Products
Technical Specifications
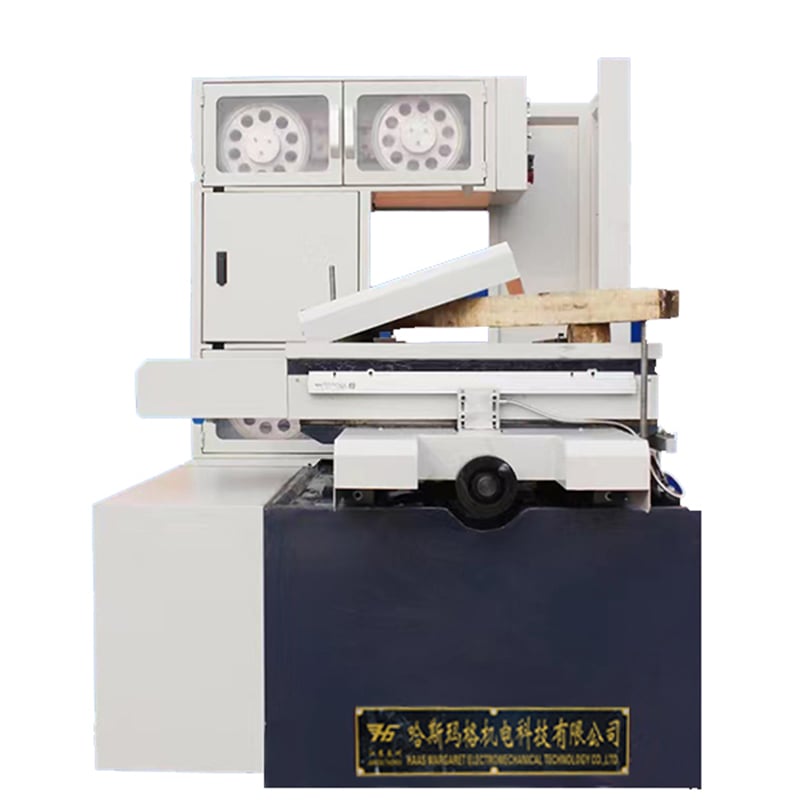
Main Technical Parameters for QT5635H
| No. | Item | Specifications |
| 1 | Axis Travel | X-axis: 350 mm Y-axis: 450 mm |
| 2 | Worktable Size (X × Y) | 400 mm × 680 mm |
| 3 | Z-Axis Feed Travel | Optional: 250 mm, 400 mm, or 500 mm |
| 4 | Machining Accuracy (Cutting Accuracy) | ±0.03 mm* |
| 5 | Mechanical Structure | X and Y axes: High-precision linear guide rails and ball screws |
| 6 | Speed | Diamond wire speed: 0–40 m/s (adjustable) |
| Programmed Feed / Cutting Rate: Material- and process-dependent; confirm by sample cut. | ||
| 7 | Auxiliary Systems | Cooling Method: Water cooling |
| Lubrication: Manual lubrication system | ||
| Diamond wire diameter: φ0.45–1.5 mm | ||
| 8 | Drive System | Stepper motor with dedicated driver |
| 9 | Power Supply | AC 380V (optional 220V), 50Hz |
| 10 | Constant Tension Device | Pneumatic control via air pump |
| 11 | Supported File Formats | G-code, 3B code |
| 12 | Control System | HL CNC control system |
| 13 | Overall Dimensions (L×W×H) | 1800 mm × 1280 mm × 2100 mm |
| 14 | Machine Weight | 1400 kg |
| 15 | Maximum Workpiece Height | To be confirmed for the selected Z-axis configuration and fixture. |
| 16 | Maximum Cutting Thickness | To be confirmed for the selected Z-axis configuration, wire path, material and contour. |
Performance and Capacity Notes
Accuracy note: The listed ±0.03 mm machining accuracy refers to cutting accuracy under defined verification conditions. Actual results depend on material grade, workpiece dimensions and contour, wire diameter and abrasive size, wire wear, tension, linear speed, programmed feed, coolant, fixturing and measurement method. Sample-cut confirmation is recommended for application-specific tolerances.
Cutting-rate note: Cutting performance depends on material grade, cut cross-section, wire diameter and abrasive size, linear speed, feed rate, tension, coolant and the required edge quality. Programmed feed rate (mm/min), actual cutting time and effective cut-area rate (mm²/min) are different measurements and should not be used interchangeably.
Z-axis and capacity note: Z-axis feed travel is the programmable travel of the feed axis. It is not the same as maximum workpiece height or maximum cutting thickness. These capacities must be confirmed for the selected Z-axis configuration, fixture, wire path, material and contour.
Machine Overview and Applications
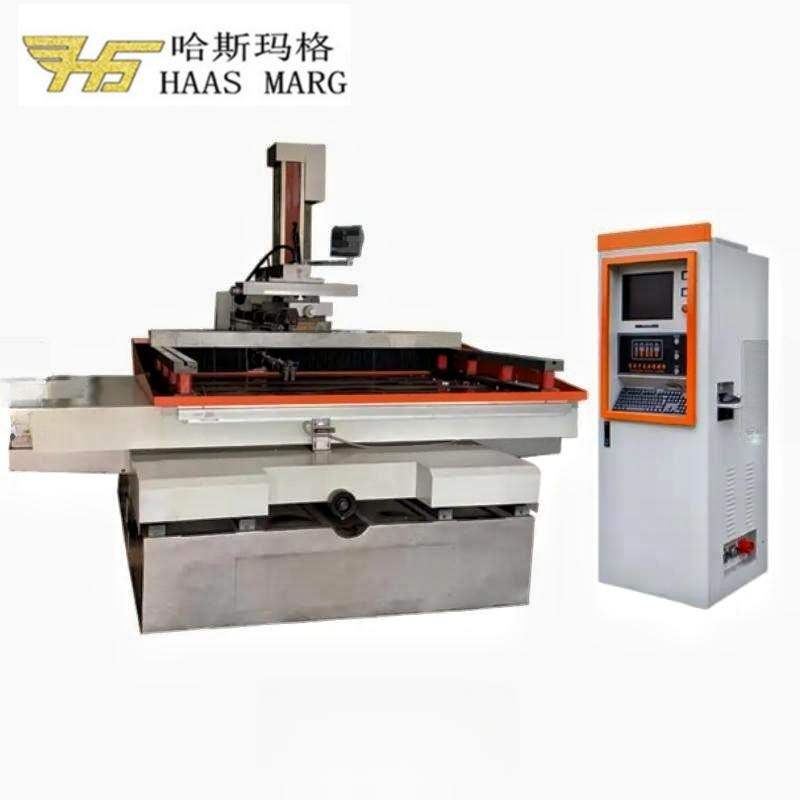
Machine Type: This H-series model is an endless-loop CNC diamond wire saw machine for precision cutting and contouring of hard and brittle materials. A closed-loop diamond wire runs continuously in one direction. Material is removed by fixed-abrasive grinding; the process is not Wire EDM and does not require an electrically conductive workpiece.
Process Characteristics: Continuous one-direction motion avoids wire-reversal events and supports the H series' higher published line-speed range. When wire specification, tension, feed, coolant and fixturing are correctly matched, it can improve cutting stability, contour consistency and productivity. Final accuracy and cycle time still require material-specific validation.
Material Groups: Applications can be evaluated for graphite; optical glass and related glass materials; technical ceramics; ferrite and other magnetic materials; semiconductor and crystal materials; and selected stone materials such as marble, jade, emerald and agate. Material compatibility and final process parameters should be confirmed by reviewing the actual drawing and, where necessary, a sample cut.
Application Note: Published machine parameters describe the equipment configuration, not one universal cutting result. Send the material grade, workpiece dimensions, contour, target tolerance and edge or surface requirement for a technical review.
Model Selection Guidance
Model Comparison: The QT5635H provides 350 × 450 mm X/Y travel with continuous one-direction endless-loop wire motion. Compare the smaller QT5632H, the larger QT5645H, or the QT5635 reciprocating model for the same listed X/Y travel. See all H-series endless-loop diamond wire saw machines.
Information Required for Technical Review
- Material and grade
- Maximum workpiece length, width, height and weight
- Straight cut, slicing or contour path, preferably with a drawing
- Target dimensional or contour tolerance, edge or surface requirement, permissible chipping and kerf
- Preferred diamond wire diameter and abrasive specification, if known
- Coolant or contamination restrictions
- Destination power supply: voltage, phase and frequency
- Required cycle time, batch size and automation or loading requirements
Training
The supplier shall provide free on-site training for 1–2 technical personnel from the buyer’s side, with a duration of 1 to 2 days.
|
No. |
Item |
Training Content |
|
1 |
Programming |
Introduction to CAM programming for diamond wire cutting |
|
Usage of G-code and 3B code |
||
|
Wire diameter compensation and path offset settings |
||
|
2 |
Operation |
Overview of machine structure and components |
|
Startup and shutdown procedures |
||
|
Control panel functions |
||
|
Program loading and parameter adjustment |
||
|
Safe operation protocols |
||
|
3 |
Mechanical Maintenance |
Part 1: Structure Overview |
|
– X/Y/Z axis motion system and guide rails |
||
|
– Wire feeding and tension unit |
||
|
– Lubrication and cooling system |
||
|
Part 2: Troubleshooting |
||
|
– Diamond wire replacement |
||
|
– Guide wheel and wire path alignment |
||
|
– Handling wire breakage or jamming |
||
|
4 |
Electrical Maintenance |
Identify key electrical components and symbols |
|
Basics of electrical circuits |
||
|
Reading control cabinet diagrams |
||
|
Fault diagnosis (motor, sensor, signal issues) |
||
|
5 |
Practical Testing |
Workpiece clamping and alignment |
|
Program dry-run verification |
||
|
Actual cutting test and monitoring |
||
|
Workpiece inspection and quality evaluation |
After-Sales Service
- From the date of delivery, the supplier provides a one-year mechanical warranty. Under normal operating conditions, the supplier is responsible for free maintenance and replacement of spare parts; however, consumable parts, wear parts, and tools are not covered under the warranty.
- After the one-year warranty period, the supplier will provide the necessary spare parts for repairs and offer repair services at reasonable charges.