Home > Products > Wire Cutting Machine > CNC Diamond Wire Saw Machines
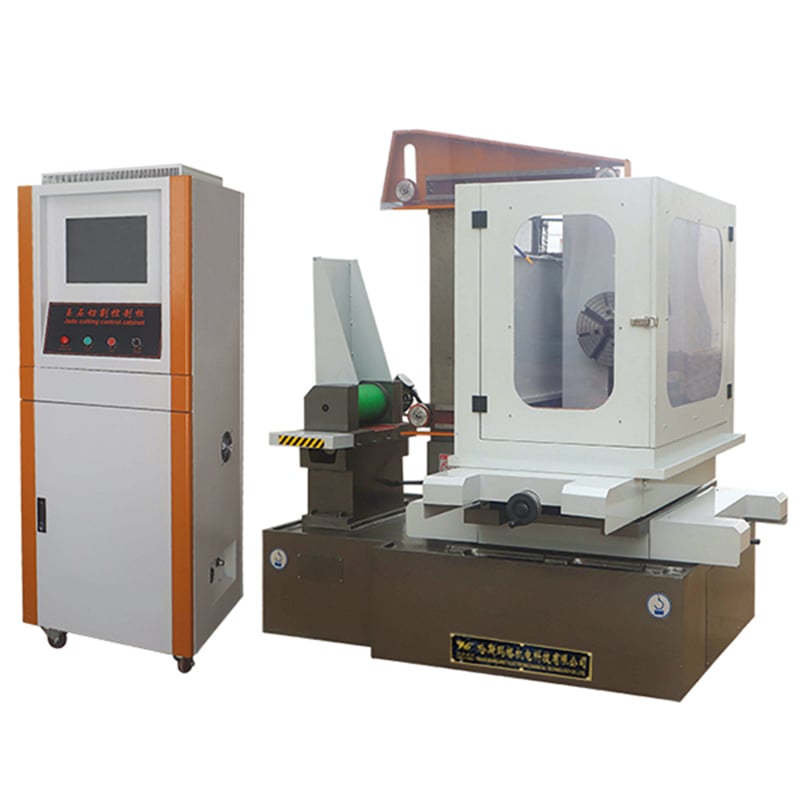
HarsMarg CNC diamond wire saw machines use fixed-abrasive diamond wire to mechanically cut and profile hard and brittle materials. Typical applications include graphite, optical glass, technical ceramics, ferrite and other magnetic materials, semiconductor and crystal materials, and selected stone products. The process removes material through abrasive grinding. It is not Wire EDM and does not rely on electrical-discharge erosion, so the workpiece does not need to be electrically conductive.
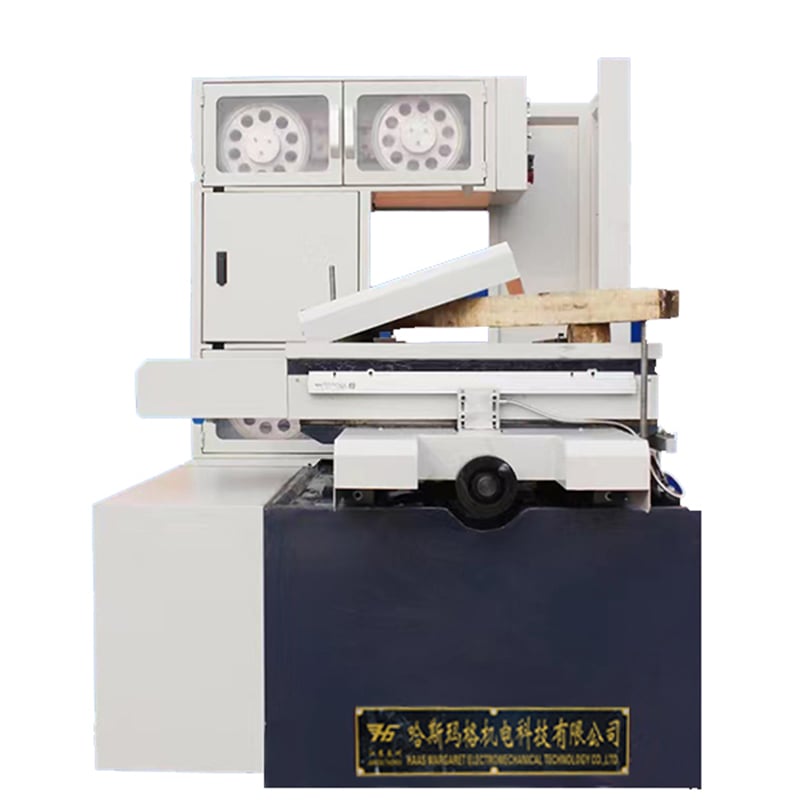
The range includes reciprocating and endless-loop machine structures. Reciprocating models store diamond wire on a wire drum and alternate the wire direction during cutting. H-series endless-loop models run a closed-loop diamond wire continuously in one direction. Continuous one-direction motion removes wire-reversal events and supports the higher published line-speed range of the H series. When wire specification, tension, feed rate, coolant and fixturing are correctly matched, this structure can improve cutting stability, contour consistency and productivity. Final accuracy, surface condition and cycle time must still be confirmed for the actual material and geometry.
| Selection Point | Reciprocating Models | H-Series Endless-Loop Models |
|---|---|---|
| Wire motion | Wire stored on a drum; direction alternates during cutting | Closed-loop wire runs continuously in one direction |
| Wire form | Diamond wire wound on a storage drum | Closed endless-loop diamond wire |
| Published wire-speed range | Up to 11.5 m/s, depending on model and configuration | Up to 40 m/s, depending on model and configuration |
| Published wire-diameter range | Model-dependent, currently listed from φ0.12 mm to φ0.45 mm | Model-dependent, currently listed from φ0.44 mm to φ1.5 mm |
| Suitable workpieces and process fit | Hard or brittle workpieces within the selected model's envelope when a drum-stored reciprocating system and the listed thinner wire range fit the job | Hard or brittle workpieces within the selected model's envelope when continuous motion, higher listed line speed and stable contour cutting are priorities |
| What must be confirmed | Material grade, workpiece size and weight, contour, target tolerance, edge and surface requirements, wire specification, coolant, fixture, power supply and required cycle time | |
Compare reciprocating diamond wire saw machines or review the H-series endless-loop diamond wire saw machines. Model selection should be based on the required X/Y travel, table size, Z-axis configuration, fixture, wire specification and process target rather than the model number alone.
The following setup is a proposed engineering starting point for application validation, not a universal production setting, a completed HarsMarg test record or a claim that every material will achieve the same result. A representative comparison can use three K9 optical-glass samples measuring 100 × 100 × 20 mm and a 60 × 60 mm rounded-square contour with R10 corners.
For a ±0.03 mm application requirement, the result should be confirmed on the customer's material and drawing. Cutting speed must be reported separately as programmed feed rate, actual cutting time and effective cut-area rate; these values should not be treated as interchangeable.
For a technical recommendation, send the material and grade; maximum workpiece length, width, height and weight; required straight, slicing or contour path; drawing and target tolerance; required edge condition, surface finish and kerf; preferred wire specification if known; coolant restrictions; destination-country power supply; and required cycle time. HarsMarg can then review the machine envelope, Z-axis configuration, fixture, wire path and sample-cut requirement before quoting.

 EN



